Frequency is the process variable that most directly changes how cavitation behaves in an ultrasonic cleaning tank. A 25 kHz system does not simply clean a little faster or slower than a 40 kHz system; it changes bubble size, collapse energy, surface stress, and the types of contaminants the tank can reliably remove. Understanding those differences helps production and quality teams avoid surface damage while hitting required cleanliness levels.
How Cavitation Turns Ultrasonic Energy into Cleaning Action
In an ultrasonic cleaning system, the generator drives transducers at a selected frequency, and the tank wall or immersion plate transmits that vibration into the liquid. The alternating pressure field creates low-pressure and high-pressure zones. During the low-pressure phase, vapor and dissolved gas form microscopic bubbles. During the high-pressure phase, those bubbles collapse, often asymmetrically near a solid surface, producing microjets and localized mechanical stress [1]. This is the primary mechanism that removes oil films, particles, and residues from blind holes, threads, and recessed surfaces. Bubble behavior is closely tied to frequency. Lower frequencies produce larger bubbles and more energetic collapse events, while higher frequencies produce smaller bubbles and more numerous but gentler implosions. That relationship explains why frequency selection is not a minor setting; it determines how aggressively the cleaning field interacts with the part material.
Before changing any process variable, it helps to understand how the generator and transducers create the acoustic field. <Qu’est-ce que la onde ultrasonique ?> covers wave behavior, transducer placement, and the acoustic field inside an industrial tank.
Low Frequency vs High Frequency: What Changes in the Tank
In industrial practice, 20–28 kHz is generally considered the low-frequency range for heavy-duty ultrasonic cleaning. The larger cavitation bubbles release more energy when they collapse, making this range effective for thick grease, carbon deposits, stamping oils, chips, and other coarse soils on steel and iron parts. The trade-off is surface stress. The same collapse energy that removes heavy contamination can also erode soft substrates, sharp edges, or thin sections if exposure time and power are not controlled [2]. Higher frequencies, typically 40–80 kHz and above, create smaller cavitation bubbles with lower individual collapse energy. The cleaning field tends to be more uniform and reaches tighter clearances with less risk of cavitation erosion. This range is often preferred for polished aluminum, brass, copper, coated surfaces, optics, and precision components. Because the bubbles are smaller, they can enter narrow gaps more easily and remove fine particles without as much mechanical impact [3].
Frequency range
Bubble and cleaning behavior
Typical production use
20–28 kHz
Larger bubbles, high-energy collapse
Heavy oil, carbon, chips on steel and iron
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Balanced bubble size and scrubbing action
General industrial ultrasonic cleaning
68–80 kHz+
Smaller bubbles, gentler and more uniform
Polished, coated, and precision parts
The table does not mean that one frequency is objectively better. It means the correct choice depends on the part, the contaminant, and the surface finish that must be preserved.
Matching Frequency to Part Material and Contaminant
Material response is as important as contaminant type. Stainless steel, titanium, and dense ceramics generally tolerate lower frequencies well, especially when the goal is aggressive degreasing or carbon removal. Aluminum, brass, copper, plated parts, and thin-wall components are more vulnerable to cavitation erosion, so they usually benefit from 40 kHz or higher unless process trials show otherwise [2]. Contaminant type should guide the selection as well. Heavy oils, greases, polishing pastes, and baked carbon require stronger mechanical action. Light oils, fingerprints, dust, and submicron particles often respond better to high-frequency scrubbing because the smaller bubbles produce a more uniform cleaning field in fine features. Multi-stage systems frequently pair a low-frequency wash tank with a high-frequency rinse tank: the first stage removes bulk soil, and the second stage improves final cleanliness without adding surface damage.
Frequency, Power, and Process Control in Industrial Systems
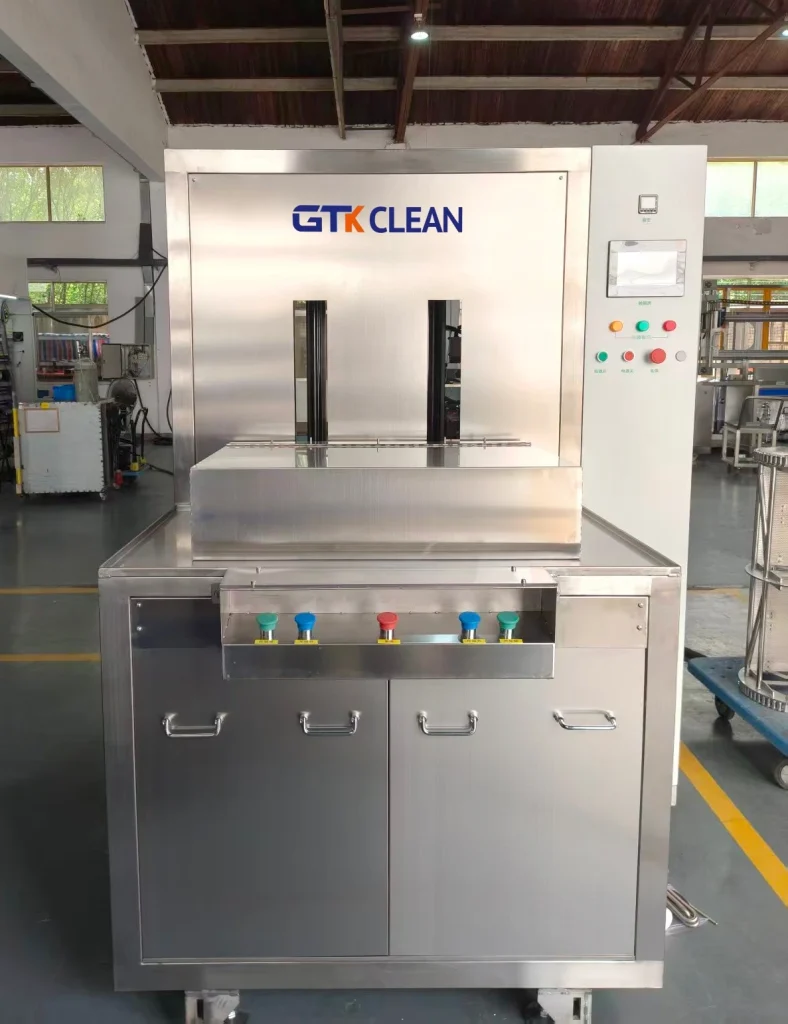
Frequency does not act alone. Power density, degassing time, temperature, chemistry, and part loading determine whether a selected frequency performs as expected. A 40 kHz tank with insufficient power density may under-clean heavy components, while a well-tuned 25 kHz system may still damage soft metals. Process control therefore matters more than any single frequency number. Modern industrial systems often use sweep or pulse modes to avoid standing waves and dead zones. Multi-frequency or selectable-frequency generators, including 20/28/40/80 kHz configurations, give process engineers flexibility when the product mix changes. As an example, GTKCLEAN benchtop ultrasonic cleaners and ultrasonic vibration plates are specified across the 20–80 kHz range for R&D trials and production tanks. Dual-frequency operation can combine coarse removal and fine cleaning in one system, but transducer bandwidth and tank geometry must be specified correctly for the field to stay uniform. If you are currently running one frequency for every part and seeing residue or surface marking, review frequency and power density together. Send your part material, contamination type, and required cleanliness level to [email protected] for a direct technical recommendation before changing equipment.
Need a Frequency-Matched Ultrasonic Cleaning System?
GTKCLEAN engineers can help you specify frequency, power density, transducer layout, and multi-tank process flow for your parts. Contact us at [email protected] or call +86 17768507147 to review your current cleaning results and define a process that balances cleaning speed with surface protection.
Questions fréquemment posées
Does lower frequency always clean faster?
Not necessarily. Lower frequency removes heavy soil more aggressively, but speed also depends on power density, chemistry, temperature, part geometry, and loading. For fine particles or delicate surfaces, a higher frequency can produce a better result in less total process time because it causes less rework or surface damage.
What frequency is safest for aluminum and brass?
Aluminum, brass, and other soft alloys usually tolerate 40 kHz or higher more safely than 20–28 kHz. The goal is to reduce high-energy bubble collapse against sensitive surfaces. Process trials with the actual part and contaminant are still recommended before locking a production setting.
Can one ultrasonic system cover multiple frequencies?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Does higher frequency remove submicron particles better?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits


 If you are currently running one frequency for every part and seeing residue or surface marking, review frequency and power density together. Send your part material, contamination type, and required cleanliness level to [email protected] for a direct technical recommendation before changing equipment.
 French
 English
 German
 Spanish
 Russian
 Portuguese