Passivation is often treated as a standalone chemical bath, but in a production line it only works after the right metal preparation sequence. Without effective cleaning, free iron, heat tint, machining residues, and rinse contamination stay on the surface and interfere with the formation of a passive oxide layer. This article explains how passivation works, where it fits in metal preparation, and which process controls determine whether parts leave the line protected and coating-ready.
What Metal Preparation Includes Before Passivation
Metal preparation is the complete sequence that makes a component chemically and physically ready for the next operation. For stainless steel and other corrosion-resistant alloys, preparation usually includes:
Removal of machining oils, cutting fluids, chips, and shop dust
Removal of oxide scale, weld tint, and heat-treatment discoloration
Removal of iron contamination smeared onto the surface by tools, fixtures, or handling
Rinsing to remove cleaning chemistry and dissolved contamination
Final drying that prevents water spots and flash rust
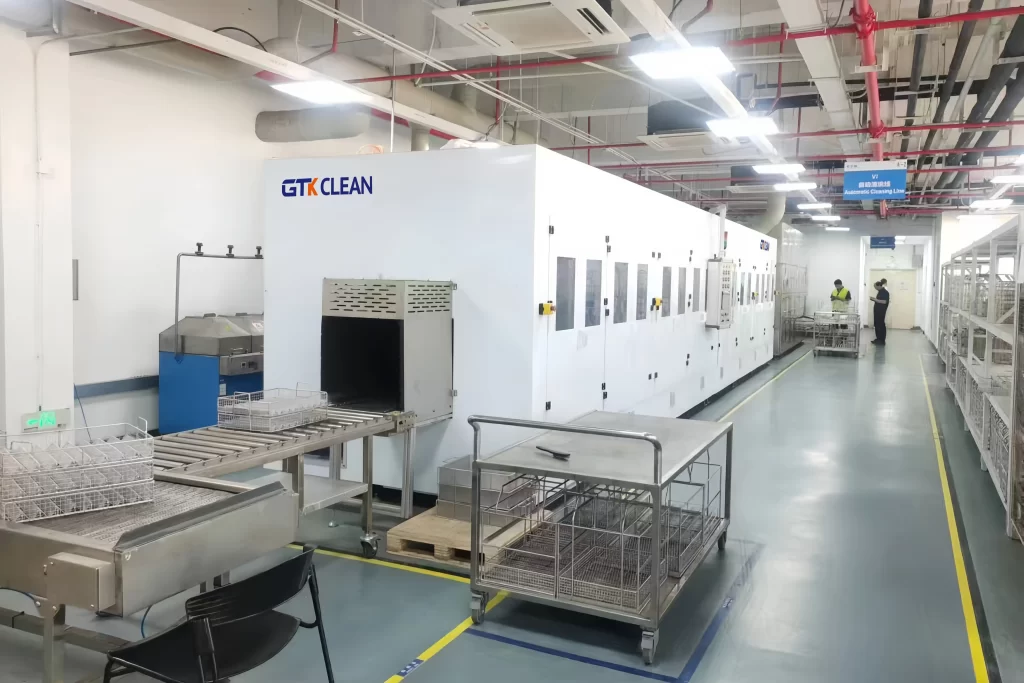
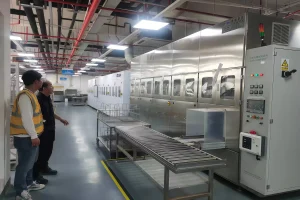
Cleaning and passivation are not interchangeable. Cleaning removes external soil; passivation removes or neutralizes surface iron and establishes a corrosion-resistant chromium oxide film. If cleaning is incomplete, the acid bath must work through oil films and heavy soil before it can reach the base metal, which produces uneven results. Effective preparation usually uses staged equipment such as spray prewash, ultrasonic cleaning, rinse tanks, and drying modules. Multi-tank systems are common because they separate each chemistry and prevent cross-contamination between cleaning, rinsing, and passivation.
What Passivation Actually Does
Passivation improves the natural corrosion resistance of stainless steel. Stainless alloys resist corrosion because chromium in the metal reacts with oxygen to form a thin, adherent, chromium-rich oxide layer. However, manufacturing operations can leave free iron on the surface. That free iron corrodes quickly and creates initiation points for pitting, staining, or coating failure. The passivation bath dissolves surface iron and other tramp contaminants while allowing the chromium oxide film to form uniformly. The acid does not remove heavy scale or weld tint; that is the role of pickling. Passivation is a relatively mild chemical treatment intended for clean parts that still carry invisible surface iron and process residues [1]. This distinction matters for metal preparation. A part with weld scale or heat tint should be pickled or mechanically descaled first. A part that is already dimensionally finished and clean can go directly to passivation.
Passivation vs Pickling vs Cleaning
The table below separates three processes that are frequently confused in surface preparation.
Processus
Main target
Chemical action
Surface result
Nettoyage
Chips, oil, grease, particulate, light residues
Detergents, solvents, spray, ultrasonic action
Visible surface free of gross soil
Pickling
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Passivation
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Nitric Acid vs Citric Acid Passivation
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Variable
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Passivation Process and Critical Control Points
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Séchage
Stage
Objectif
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Prevent mineral deposits and chloride residues
Conductivity or resistivity, pH, rinse time
Séchage
Prevent flash rust and water spots
Part temperature, air cleanliness, drainage
Water quality is one of the most underrated variables. A final rinse with hard water or chloride-containing water can leave spots and corrosion cells on a passivated surface. ASTM A380 addresses cleaning and passivation of stainless steel parts and systems, including the importance of clean, low-chloride rinse water [3]. In precision applications, the final rinse should be dbuy deionized water with controlled conductivity and adequate overflow. Passivation verification is part of the process, not an afterthought. ASTM A967 lists tests such as water immersion, high-humidity exposure, salt spray, copper sulfate, and ferroxyl testing [1]. The appropriate test depends on the part risk level, material grade, and customer requirement.
Common Passivation Failures and Preventive Measures
Most passivation problems are not caused by the acid bath alone. They trace back to preparation, rinsing, or handling.
Failure
Typical cause
Preventive action
Flash rust after passivation
Poor rinsing, contaminated final rinse, wet storage
Use clean DI rinse, dry immediately, protect parts from humid air
Etching or pitting
Excess acid concentration, high temperature, long immersion
Control bath parameters, verify grade and part condition
Water spots
Hard water or mineral-laden final rinse
Use deionized water, overflow rinsing, controlled drying
Uneven passivation
Oil or residue on part, trapped air in blind holes
Improve precleaning, use agitation or fixturing
Copper sulfate test failure
Free iron not fully removed
Check bath life, temperature, time, and surface cleanliness
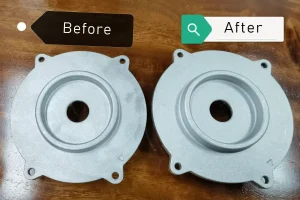
Blind holes, threads, and narrow gaps require particular attention. These features trap cleaning chemistry, acid, or rinse water, and they can carry contamination into the passivation bath. Basket design and part orientation should promote drainage at every stage. A washing basket that holds parts too tightly or blocks internal features can create isolated areas that never see proper flow.
How Cleaning Equipment Supports Repeatable Passivation
Passivation is highly sensitive to surface consistency. Manual cleaning may be acceptable for low-volume or simple parts, but production lines with mixed part numbers benefit from automated multi-stage equipment. Automation controls soak time, rinse time, temperature, and transfer, reducing the variation that causes lot-to-lot passivation failures. A pre-coating ultrasonic cleaning line, for example, may combine spray prewash, ultrasonic degreasing, multi-stage ultrapure water rinsing, and hot-air or vacuum drying. In one GTKCLEAN pre-PVD system design, the ultrapure water system targets conductivity of 0.06 µS/cm or less to prevent water spots and secondary contamination before coating. That same control logic applies to passivation lines: the cleaner the surface before chemical treatment, the more uniform the passive film.
If you are specifying a passivation stage or updating a manual wash line, send your substrate, part geometry, contaminants, and required cleanliness standard to [email protected]. Engineering can review the sequence and recommend where ultrasonic cleaning, DI-water rinsing, and passivation should sit in the line.
Engineering Support for Passivation and Metal Preparation
A reliable passivation process starts with a cleaning line that delivers the same surface condition batch after batch. For an engineering review, contact GTKCLEAN with the following information:
Part material and grade, such as 304, 316L, or 17-4 PH
Contamination present before cleaning: oil, chips, scale, rust, fingerprints, or polishing compound
Part geometry, including blind holes, threads, and internal cavities
Required throughput, basket load, and part weight
Next process after cleaning: coating, welding, assembly, or storage
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
FAQ
Is passivation the same as pickling?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Can carbon steel be passivated?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
Does passivation remove machining oil?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
What final rinse water quality is needed?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits
How is passivation verified?
cURL Too many subrequests by single Worker invocation. To configure this limit, refer to https://developers.cloudflare.com/workers/wrangler/configuration/#limits


 French
 English
 German
 Spanish
 Russian
 Portuguese