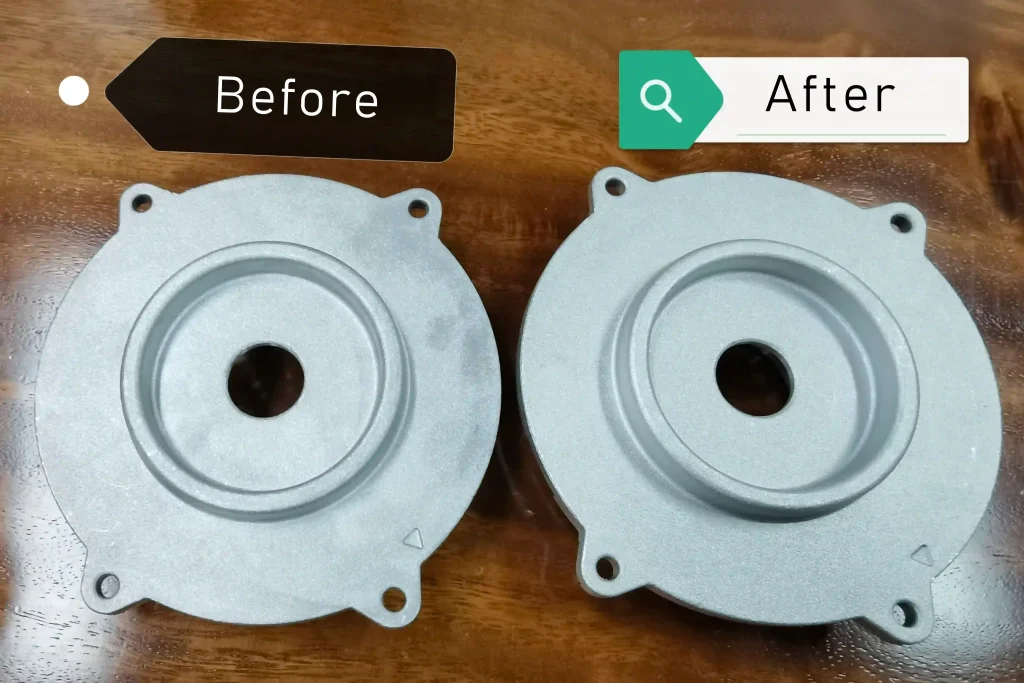
Die Nachbearbeitungsreinigung ist der Punkt, an dem ein Bearbeitungsprozess sich entweder bewährt oder ein Problem an die nächste Stufe weitergibt. Das häufigste Versagen liegt nicht an der Waschanlage selbst; es ist eine Linie, die um den Tank herum konzipiert ist, anstatt um die Spänebelastung, die Kühlmittelchemie und die nächste Operation. Das zuverlässige Entfernen von Spänen und Kühlmittel nach CNC-Bearbeitung bedeutet, den Schritt als Prozessgrenze zu behandeln, nicht als Waschanlage. Ein bearbeitetes Teil verlässt die Maschine mit losen Spänen, verpackten Spänen in Blindlöchern und einem Kühlmittel-Film, der aushärten oder reagieren kann, wenn die Sequenz ihn nicht sauber entfernt.
Warum scheitert die Reinigung nach der Bearbeitung, bevor der Wascher startet?
The parts arriving at the cleaning line are not the same parts shown in the equipment layout. One batch can carry long stringers, another fine compacted chips, another a coolant that has begun to separate under heat. When the line is sized around a clean part in a basket, every real contaminant becomes a downstream surprise. Two decisions cause most failures. The first is applying heat before mechanical removal. A heated tank bakes wet coolant into a film and turns loose chips into a bonded deposit. The second is trusting one stage to do the work of three: knock down the bulk, dissolve the film, and rinse the surface. I have watched a production line load wet chip-laden baskets directly into a heated tank and then struggle with baked fines in the corners of every part. The fix was not a stronger detergent; it was moving chip separation ahead of the heated stages so the downstream tanks were not trying to remove a cured layer.
Wie entfernt man Späne und Kühlmittel von der Maschinenseite?
Loose chips should not get a chance to settle. A high-pressure spray stage immediately after machining, before the parts enter a heated tank, removes the bulk of chips and keeps most of them out of the filtration loop. The spray does not need to make the part clean. It needs to stop the main contaminant load from turning into paste. For blind holes and cross-drillings, orientation does more than spray pressure. If the hole stays upright, gravity works against the process and the jet can push chips deeper. Rotating the basket or tilting the part lets the wash fluid flush chips out and drain them before the next stage.
Wann macht ein rotierender Korb Sinn?
A rotary basket makes sense when a part has blind holes, cross-drillings, or recesses that hold chips in more than one plane. The rotation moves fluid through the feature and lets it drain. Flat parts in a static basket often need no rotation, and the simpler orientation makes high load density easier. Coolant should also be treated as a contaminant, not a lubricant for the cleaning line. Water-soluble emulsions that enter a solvent rinse or a rinse tank can contaminate the following stages. That is why the machine-side spray should be combined with a dedicated first-stage collection system instead of carrying over into the ultrasonic tank.
Welche Wasch-, Spül- und Trocknungssequenz passt zum Teil und zur nächsten Operation?
The wash sequence starts with the coolant chemistry and ends with the next operation. A water-soluble coolant is not the same cleaning problem as a neat cutting oil, and a part going to assembly is not the same problem as a part going to coating. | Coolant type | Residue behavior | Better first wash stage | Reason |
| Water-soluble | Emulsion film with fines | Alkaline aqueous at 45 to 65 °C | Breaks the emulsion and suspends fines |
| Semi-synthetic | Waxy film after water leaves | Alkaline aqueous plus agitation | Needs heat and movement to saponify the film |
| Neat cutting oil | Viscous oil film | Hydrocarbon or modified alcohol solvent | High solvency with low surface tension |
| Chlorinated EP coolant | Sticky sulfur and chlorine film | Solvent with vacuum or strong aqueous | Needs sustained contact and controlled temperature |
| Dried-on coolant | Hardened coating | Solvent pre-soak then ultrasonic | Aqueous alone cannot lift a cured film quickly | Temperature matters because solubility changes with the coolant, not just the detergent. A hydrocarbon solvent system cleans stamping and cutting oils best between 40 and 60 degrees Celsius, while an aqueous alkaline stage often runs from 45 to 65 degrees Celsius. Those ranges are starting points, not guarantees; a wash trial with the actual coolant is the only way to confirm contact time and concentration. The rinse is the part most buyers compress. If the final rinse is not low-mineral water, the part will dry with water spots that become defects in the next operation. We specify ultrapure water at no more than 0.06 microsiemens per centimeter for pre-coating and precision lines because stray minerals are hidden residue. If your parts combine blind holes with chlorinated extreme-pressure coolant, the wash chemistry and drying sequence are worth confirming before you finalize the line. We can check the process against your part drawing and coolant SDS at [email protected].
Die Wahl eines Waschers für CNC-gefertigte Teile hängt ebenso vom Kontaminantentyp wie von der Teilgröße ab. <Auswahl industrieller Teilewascher für den Erfolg beim CNC-Bearbeiten> beschreibt, wie Waschstufen, Korbbewegung und Filtration auf die Späne- und Kühlmittelbelastung abgestimmt sind.
Wie überprüft man die Ergebnisse der Nachbearbeitungsreinigung?
A line that looks clean in the tank can still leave residue in a blind hole or water in a cross-drilling. Verification has to happen at the part, not at the machine status screen. The simplest checks are still useful: wipe a white cloth across the surface, run a water break test, and inspect the worst feature on the part before the basket moves on. Process control keeps those checks repeatable. Temperature, stage time, rinse conductivity, and detergent concentration should be monitored and alarmed. If the rinse water drifts above its conductivity limit, the line is no longer producing the same cleanliness, even if the cycle time has not changed. For critical parts, we add periodic particle counts and a defined sample plan. The key is not to measure everything; it is to define the few failure modes that matter for the next operation and check those the same way each shift.
Wie sollte eine Schichtüberprüfung aussehen?
Mindestens sollten die Reinigungstemperatur, Rinse-Leitfähigkeit, Zykluszeit und eine visuelle Kontrolle des schwierigsten Merkmals an einem Probe-Teil erfasst werden. Wenn die Linie automatische Alarme hat, verwenden Sie diese, um Quarantäne auszulösen, anstatt Teile nachträglich zu sortieren. Ein stabiler Datensatz erleichtert es, ein Beschichtungs- oder Montageproblem auf die Reinigung zurückzuführen oder die Reinigung auszuschließen.
Was sollten Sie tun, bevor Sie eine Nachbearbeitungsreinigungsanlage kaufen?
Die meisten Probleme bei der Nachbearbeitung nach dem Bearbeiten werden nicht durch den Kauf eines größeren Waschers gelöst. Sie werden durch die Prozesssequenz um die tatsächliche Späne- und Kühlschmierstoffbelastung gelöst. Bevor Sie die Geräte liste reparieren, senden Sie die Teilezeichnung, Material, Spänetyp, Kühlschmierstoff-SDS, wöchentliches Volumen und die nächste Operation. Diese Informationen reichen aus, um zu prüfen, ob die Linie mit Sprühen, Lösungsmittel oder Ultraschall beginnen sollte und welche Trocknungsmethode Bestand hat. Kontaktieren Sie uns unter [email protected] oder +86 17768507147, und wir erarbeiten gemeinsam die Prozesssequenz.
Was fragen Käufer sonst noch zum Entfernen von Spänen und Kühlmittel?
Funktioniert Ultraschallreinigung sowohl für Späne als auch für Kühlmittel?
Ja, aber nur, wenn das System richtig vorbereitet ist. Ultraschallkavitation entfernt feine Partikel und Kühlschmierstofffilme von komplexen Oberflächen, einschließlich Blindlöchern und Gewinden, ist aber nicht der erste Schritt bei schweren losen Spänen. Ein Hochdrucksprüh- oder mechanischer Späneentfernungsabschnitt sollte die Hauptladung zuerst tragen. Wenn Kavitation nach dem Sprühen eingesetzt wird und mit der richtigen Chemie kombiniert ist, erreicht sie Stellen, die manuelles Abwischen nicht erreicht. Die Generatorfrequenz und die Leistungsdichte sind ebenfalls wichtig; niedrigere Frequenzen sorgen für stärkeren Schrubben bei harten Filmen, während höhere Frequenzen feinere Oberflächen schonender reinigen.
Kann ich die Trockenphase überspringen, wenn der nächste Prozess nass ist?
Das Überspringen der Trockenphase scheint eine kostensparende Maßnahme zu sein, verschiebt das Problem jedoch meist in den nächsten Schritt. Wasser, das in Blindlöchern verbleibt, kann Kühlschmierstoffe in einem späteren Bearbeitungsschritt kontaminieren, die Montage- oder Schmiermittel beeinträchtigen oder bei Hitzeeinwirkung sprühen. Ein nasses Teilegestell ist auch schwerer zu handhaben und kann Rinse-Wasser in die Verpackung tragen. Wenn der nächste Prozess wirklich nass ist, reicht eine teilweise Entwässerung möglicherweise aus, aber nur, wenn das Wasser nicht eingeschlossen werden kann. Für die meisten CNC-Teile sind Heißluft- oder Vakuumtrocknung obligatorisch.
Wie erkenne ich, ob die Anlage mein Produktionsvolumen bewältigen kann?
Es hängt davon ab, wie viele Körbe pro Stunde benötigt werden und wie viel Spänebelastung jeder Korb trägt. Das Volumen ist nicht nur die Stückzahl; es ist die Kontaminantenmasse, die die erste Stufe entfernen muss, und die Trocknungszeit, die die letzte Stufe abschließen muss. Ein hochvolumiges Teil mit tiefen Löchern benötigt möglicherweise mehr Tanks oder eine Tunnelkonfiguration, während eine kleine, gemischte Charge in einer halbautomatischen Mehrtanklinie laufen kann. Bitten Sie den Lieferanten, die Zykluszeit anhand Ihres schlimmsten Falls zu berechnen, nicht anhand des einfachsten. Berücksichtigen Sie Lade- und Entladezeiten in dieser Berechnung.
Wann ist die Lösungsmittelreinigung besser als die wässrige Reinigung nach der Bearbeitung?
In Linien, die für saubere Schneidöle vorgesehen sind, gewinnt die Lösungsmittelreinigung oft bei der Trocknungszeit, weil das Lösungsmittel eine schnell trocknende Oberfläche hinterlässt, während wässrige Systeme heißer Luft und manchmal Vakuum benötigen, um Vertiefungen zu trocknen. Wasserbasierte Systeme funktionieren jedoch weiterhin gut für viele wasserlösliche Kühlschmierstoffe, insbesondere wenn der nächste Schritt Galvanisieren oder Schweißen ist. Die Wahl hängt vom Kühlschmierstoff, der Geometrie des Teils und der nachgelagerten Toleranz für Wasserflecken oder Lösungsmittelrückstände ab. Senden Sie Ihre Teilegeometrie, Kühlschmierstofftyp und Zielreinheit an [email protected], und wir können vor Ihrer Entscheidung die passende Sequenz bestätigen. Automatisierter TunnelreinigerOptimieren Sie die Ultraschallfrequenz für verschiedene Materialien


 The rinse is the part most buyers compress. If the final rinse is not low-mineral water, the part will dry with water spots that become defects in the next operation. We specify ultrapure water at no more than 0.06 microsiemens per centimeter for pre-coating and precision lines because stray minerals are hidden residue. If your parts combine blind holes with chlorinated extreme-pressure coolant, the wash chemistry and drying sequence are worth confirming before you finalize the line. We can check the process against your part drawing and coolant SDS at [email protected].
 German
 English
 Spanish
 French
 Russian
 Portuguese